Every dust control plan comes down to two families of tools. You can keep dust from becoming airborne in the first place — wet suppression — or you can capture it after it goes airborne and filter it out — dry collection. Plants argue about which is “better,” but that is the wrong question. Each one fits certain points in the process and fails at others. The right plan for most operations uses both, deliberately.
How the two approaches actually differ
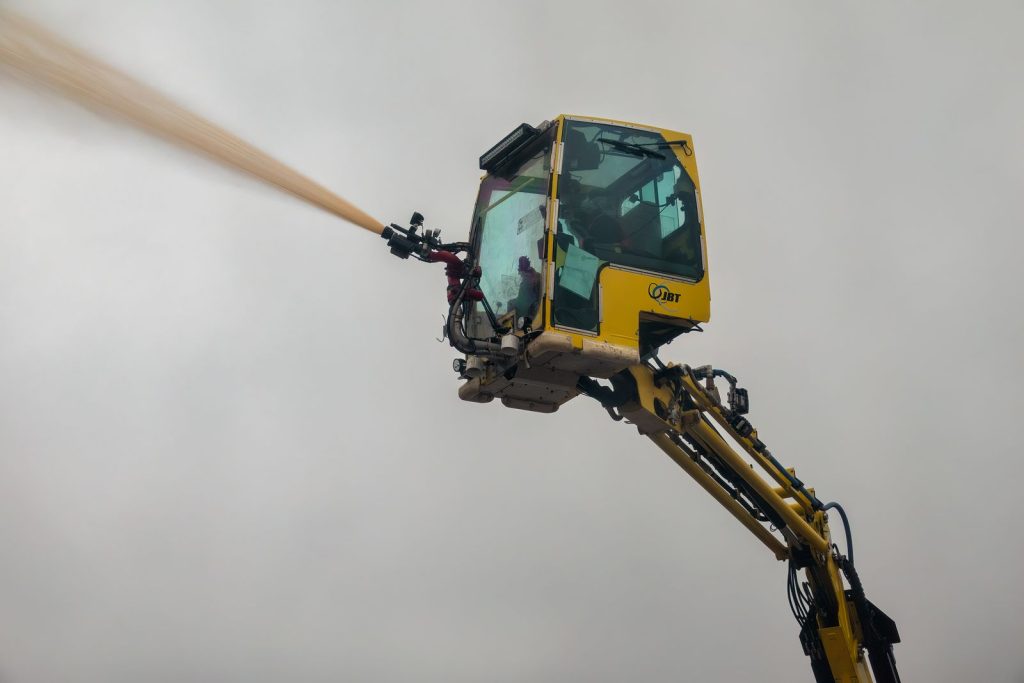
Wet suppression adds moisture to the material stream so fine particles stick to larger ones instead of taking flight. Plain water spray is the simplest form. Foam systems stretch the same water further by increasing surface coverage, and surfactant additives help water wet fine, dusty material it would otherwise bead off of. Suppression treats the material itself — the dust never leaves the rock.
Dry collection accepts that dust will go airborne at a given point, then encloses that point, pulls air through it with a fan, and strips the dust out with a baghouse or cartridge collector. Collection treats the air. The dust is removed from the process and ends up in a hopper as a separate waste or product stream.
The practical differences follow from that:
- Suppression is low capital, low complexity — pumps, nozzles, plumbing. Collection is a capital project — hoods, ductwork, collector, fan, discharge handling.
- Suppression adds water to your product. Collection does not.
- Suppression works outdoors and on mobile equipment where ducting is impossible. Collection needs fixed points it can enclose.
- Collection removes the dust permanently. Suppression only holds it down — over-dried material downstream can dust again.
Where wet suppression fits
Suppression earns its keep at the front of the plant, where material is coarse, wet tolerance is high, and enclosure is hard:
- Primary crushers. High dust generation, big open feed openings, and material that will see more processing anyway. Sprays at the feed and discharge are standard practice.
- Truck dumps and hopper feeds. Nearly impossible to enclose well; a curtain of spray or foam at the dump point is often the only practical control.
- Haul roads and stockpiles. Water trucks and stockpile sprays remain the tool of choice for open-area fugitive dust.
- Scalping and coarse screening, where a little added moisture does not hurt the process.
The craft in suppression is in the details: droplet size matched to the dust (fine dust needs fine droplets), nozzles placed where the material breaks and drops rather than sprayed generally at the pile, and enough — but no more — moisture. Overwatering causes screen blinding, chute buildup, and belt carryback, which is how suppression systems get turned off by operators and quietly abandoned.
Where dry collection fits
Collection is the tool for points where water is unwelcome or where dust must actually be removed from the workplace air:
- Screens and screen towers. Screening is a huge dust generator, and wet material blinds screen decks. Enclose and vent.
- Conveyor transfer points. Well-sealed transfer chutes with proper skirting, vented to a collector where needed, are the backbone of a dry plant’s dust control.
- Loadout spouts, silos, and bin vents. Enclosed by nature, dry by requirement — these are collection applications, full stop.
- Indoor work areas where the goal is what workers breathe, not just what neighbors see. Suppression knocks down visible dust; collection actually takes respirable particles out of the air people occupy.
The California water question
In Southern California, water is not a free input. Drought-year restrictions, the cost of trucked or metered water, and permit conditions on water use all push against suppression-heavy strategies. Foam and surfactant systems help — they deliver control with substantially less water than plain sprays — but the direction is clear: California plants tend to lean harder on sealing, enclosure, and dry collection than the same plant would in a wetter state, and to save their water for the points where nothing else works, like truck dumps and haul roads.
There is also a maintenance angle: hard water plugs nozzles. If your suppression system depends on fine-orifice nozzles and your water is untreated, plan for filtration and a nozzle-cleaning routine, or the system will quietly stop working between inspections.
When the product cannot get wet
Some processes simply veto suppression:
- Asphalt plants cannot tolerate moisture in aggregate feed beyond tight limits — every point of moisture is fuel burned in the dryer, and hot-side dust control is a baghouse application by definition.
- Cement and lime hydrate on contact with water. Suppression on clinker, cement, or lime handling is off the table; these are enclosure-and-collection materials throughout.
- Dry-rated products. If you sell material against a moisture spec — dried sand, some specialty aggregates — added water downstream of the dryer is money evaporating.
Ready-mix plants sit in the middle: aggregate moisture is measured and batched around, so modest suppression on aggregate handling is workable, but cement silo and weigh-batcher venting is strictly dry collection.
Using both — on purpose
The pattern that works at most aggregate and cement operations looks like this: suppress at the front (truck dump, primary crusher, haul roads), seal and collect through the middle and back (screens, transfers, silos, loadout). Moisture added early largely does its work before the material reaches moisture-sensitive steps, and collection handles the points where water was never an option.
Two rules make the combination work. First, treat transfer point sealing as its own discipline — a properly skirted, enclosed transfer point reduces the load on both strategies and is often the cheapest control in the plant. Second, mind the interaction: material wetted upstream sheds moisture as it moves, and a collector serving a damp airstream will blind bags. Locate collection points and choose media with the upstream water in mind.
The silica compliance angle
Regulators care about respirable crystalline silica — the invisible fraction — and both OSHA’s general industry standard and MSHA’s rule are built on a PEL of 50 µg/m³ with an action level of 25 µg/m³. Two implications for the wet-versus-dry choice:
- Visible dust knocked down is not the same as respirable dust removed. Suppression helps real exposures when it is engineered for fine particles, but only personal air sampling tells you whether a suppressed source is actually under the limit.
- Both approaches count as engineering controls, which is what the standards expect before respirators. What matters to a compliance officer is measured exposure, so whichever mix you choose, sample and document.
Putting numbers to it
The decision gets much easier once you list your dust sources and ask three questions at each one: can this material tolerate water here, can this point be enclosed and vented, and how close do people work to it? For the collection side of the ledger, our free online dust collection system designer tool lets you rough out airflow and collector sizing for your own pickup points before you talk to anyone.
For the rest, The ACT Group has been designing dust control for Southern California aggregate, cement, ready-mix, and asphalt plants from our Fontana shop for over 30 years — transfer point systems, dust collectors, and baghouse service under one roof. If you are weighing wet against dry at a specific plant, we are glad to walk the flow sheet with you and mark up where each one belongs.